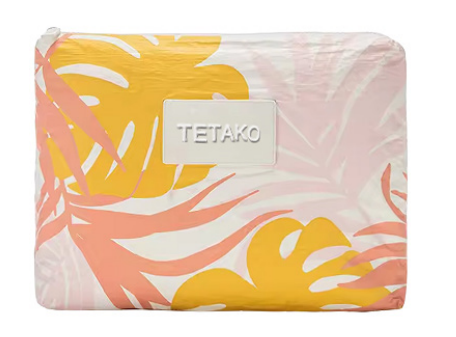
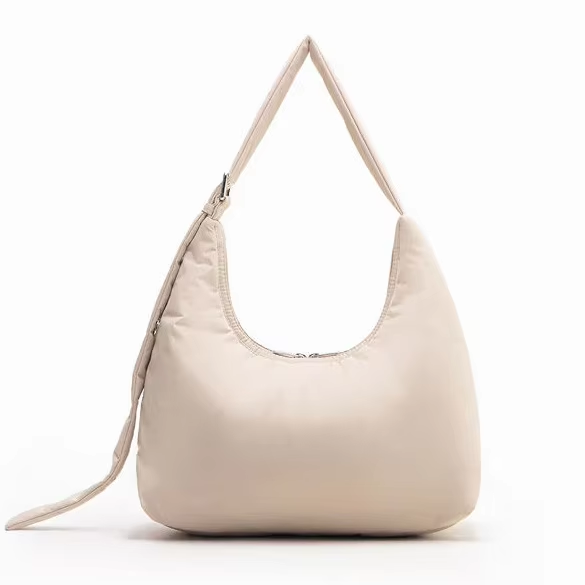
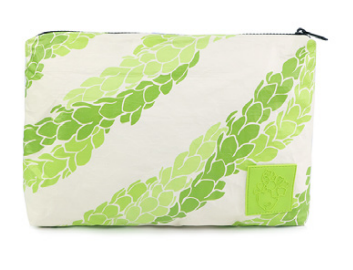
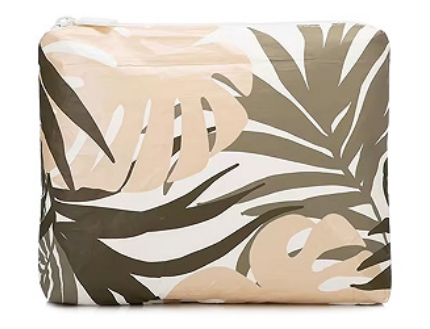
Tyvek pouches are revolutionizing the packaging industry with their unique properties and versatile applications. Manufactured from high-density polyethylene fibers, Tyvek is known for its lightweight yet robust characteristics, making it an ideal choice for businesses seeking durable packaging solutions. Our production process emphasizes quality control at every stage, from design to delivery. Each Tyvek pouch is crafted to meet the specific needs of our clients, ensuring that they receive a product that not only protects their goods but also enhances their brand image.
At Shenzhen Allwin Bags Co., Ltd., we combine over a decade of manufacturing expertise with a professional R&D team of 10-plus in-house designers. Our modern 2,000-square-meter facility with over 200 skilled workers and state-of-the-art equipment ensures precision in every cut, seam, and finish. We hold BSCI, CE, CPC, ISO, PSE, and REACH certifications, reflecting our commitment to quality assurance, social responsibility, and environmental compliance.
The innovative design of Tyvek pouches allows for customization in size, shape, and printing options, making them suitable for various industries including pharmaceuticals, e-commerce, and food packaging. We offer logo applications such as screen printing, heat transfer, and UV printing, plus special design adaptations to suit specific requirements. With a monthly production capacity of 500,000 units, we efficiently handle both small custom orders and large-volume bulk requirements.
Our commitment to sustainability means our Tyvek pouches are fully recyclable, offering an environmentally friendly choice for businesses. Samples are ready in 3 to 5 working days, bulk orders in 30 to 45 days, with flexible shipping via sea, air, DHL, FedEx, or UPS. We accept T/T and credit card payments. Our experienced team is dedicated to providing efficient and flexible solutions, quickly adapting to customer needs and market trends. By choosing our Tyvek pouches, businesses can benefit from superior protection, sustainability, and cost-effectiveness, paving the way for a brighter future in packaging.